Heterogeneous catalyst engineering ⇒ from stable and deactivation resistant to viable technical catalyst


Catalysis engineering (HCE)

Heterogeneous catalyst engineering: from stable, deactivation-resistant active phases to viable technical catalysts. We design catalysts that remain active under industrial conditions and can be manufactured at scale, from the active site to the shaped particle. Stability, scalability, and transport inside the particle are design targets from the start, not properties checked at the end. We work on thermal, photothermal, electro- and bioelectrochemical catalysts.

Problem statement. Changes in the structure of a heterogeneous catalyst are made to improve its function: activity, selectivity,y and stability. Linking structure and function requires synthesis protocols that control surface properties and porosity, identification of the active sites, mechanisms, and computational analysis.

Advances in materials science produce more active catalysts. A more active catalyst is usually more prone to deactivation and more likely to be limited by mass and heat transfer. Many advanced catalysts do not reach application because their stability under industrial conditions, with impurities, and the scale-up of their formulation were not part of the design.

The active phase also cannot be used directly in a reactor. Mechanical strength, heat and mass transport, rt and fluidization behavior require mixing it with binder and filler and shaping it into a technical catalyst [201].

Our approach, scale by scale. Our catalysts should (i) keep their stability under industrial conditions, (ii) be scalable with earth-abundant elements, and (iii) connect atomic design with reactor performance. The video zooms from the plant into a single active site, and each paragraph below matches one scene.

1. Process: activity over months. Industrial reactors run for months with heat, pressure, and impurities such as sulfur, chlorine, aromatics, and water. A catalyst has to remain active over that time, not only on day one. Stability under these conditions is the criterion we use to select formulations.

2. Reactor: the catalyst is a shaped body. Inside the reactor, the catalyst is an extrudate in a packed bed or a microsphere in a fluidized bed. The shape sets pressure drop, attrition, heat transfer, and access of reactants to the active phase [201].

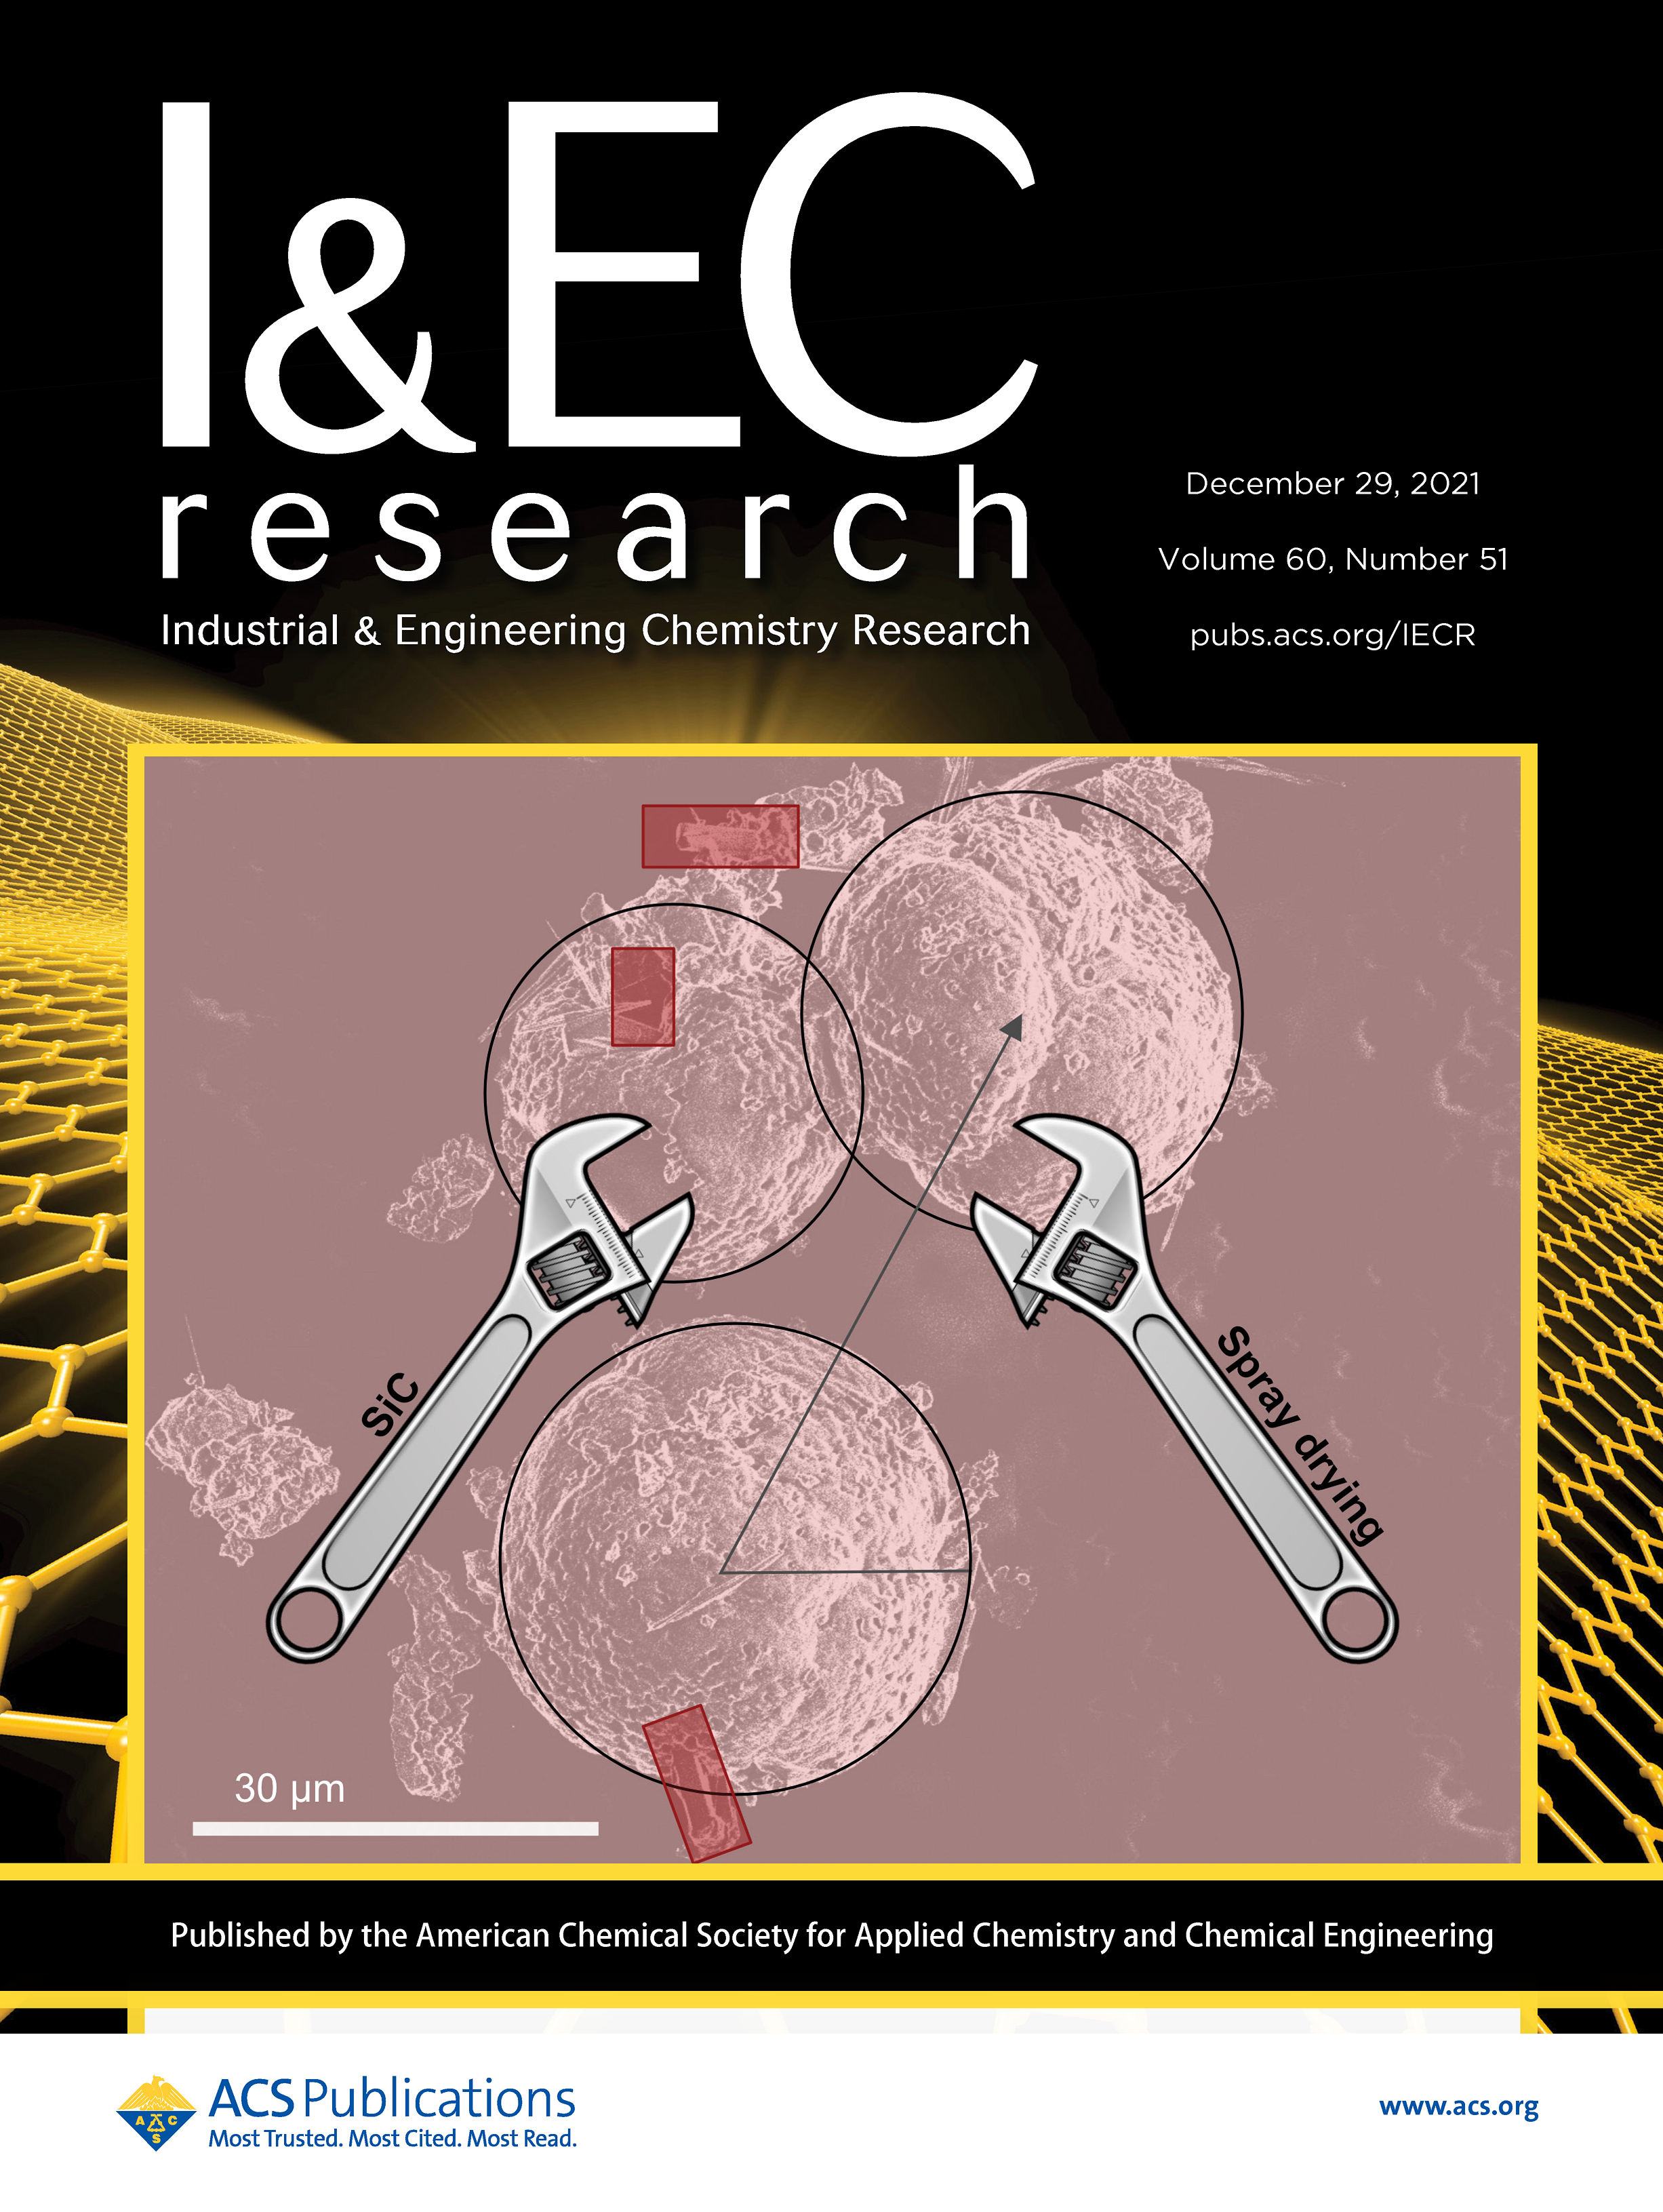
3. Particle: the technical catalyst. A technical catalyst combines the active phase with binder, filler and, in our case, silicon carbide (SiC) [131] . SiC conducts heat out of the particle in exothermic reactions such as oxidative coupling of methane [113, 121] and into it in endothermic reforming, where it also reduces coking [132, 144] . We shape particles by:

  • spray drying and extrusion [113, 144] ;
  • spray fluidized bed, for particles of 100 to 200 µm, a size range other methods do not cover well [164, 188, 204] ;
  • electrospinning.

4. Crystal: confinement of the active sites. We support and encapsulate active sites in hosts that limit sintering and coke growth:

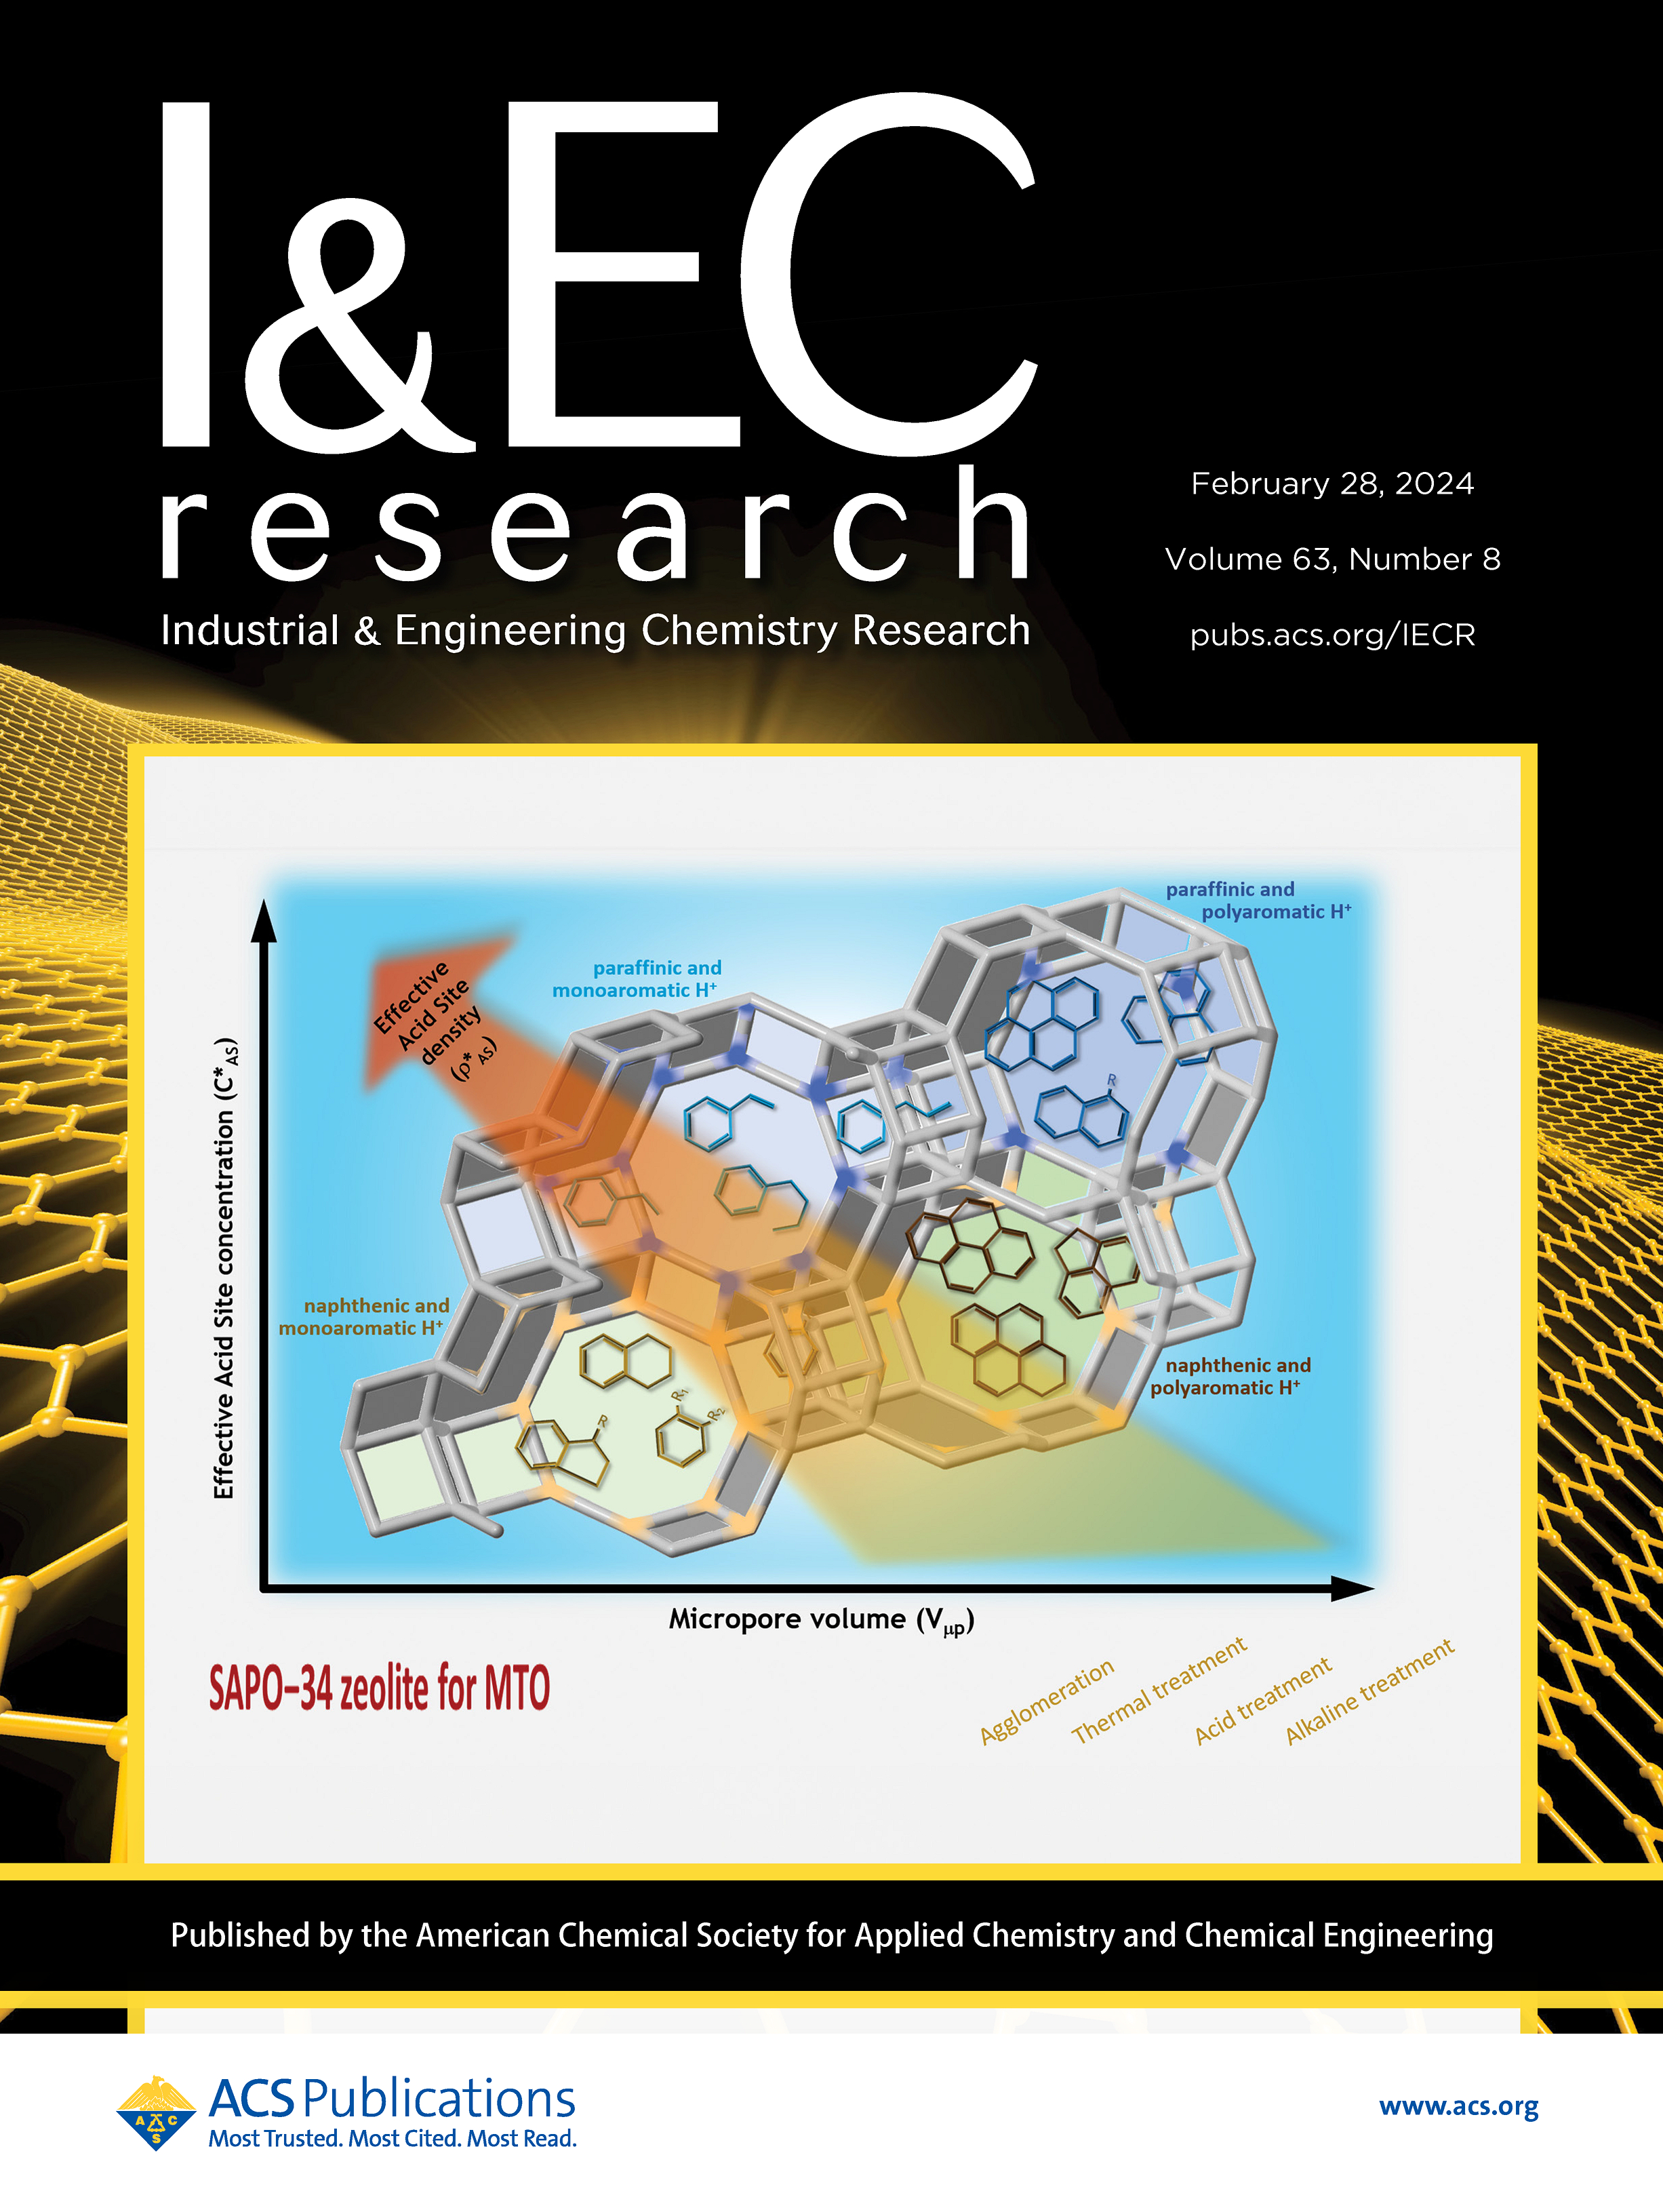
  • zeolites, including hierarchical and hollow ZSM-5 with framework-bound or encapsulated Ni for ethylene oligomerization [122, 151, 198, 208] and modified Zn/ZSM-5 for methanol to aromatics [169, 202] ;
  • metal-organic frameworks, with Cu and Pd encapsulated in ZIF-8 that remain stable in CO2 hydrogenation [163, 178, 182] , and MOFs used as precursors of Cu-Zn alloys [210] ;
  • exsolved perovskites for dry reforming of methane and crude oil reforming [136, 166, 183] ;
  • MXenes and graphene for electro-, photo- and bioelectrochemical systems [133, 135, 174, 192, 199, 207] .

5. Active site: alloys and interfaces. At the nanoscale, alloys and interfaces set the binding strength of reactants and intermediates. Examples are Ni-Fe, Ni-Zn, Ni-Ti and high-entropy alloys for dry reforming, where carbon must be removed before it grows [136, 150, 157, 205] , Cu-Ga and Cu-Zn for CO2 hydrogenation [127, 191, 210] , and metal sulfides for H2S decomposition to H2 [180] . Stability is a design target, verified under industrial conditions.

Goals. Our goals are grouped into these lines of work:

  • Technical catalyst I: spray drying and extrusion, with formulation (binder, filler, SiC) linked to activity, stability, heat transfer, and strength.
  • Technical catalyst II: spray fluidized bed granulation and coating, aggregation kinetics, and layered particles for fluidized and circulating reactors.
  • Technical catalyst III: electrospinning.
  • Zeolite catalysts with defined structure and porosity, including hierarchical and hollow zeolites with encapsulated metals.
  • Multi-metal and high-entropy alloy catalysts.
  • MXene catalysts, single- and multi-dimensional, for electro- and bioelectrochemical reactors.
  • Perovskite catalysts, including exsolved metal nanoparticles.
  • Metal-organic framework catalysts with encapsulated metal sites.
  • Supported metal and metal-oxide catalysts.
  • Aerogel catalysts.

Applications. We apply this competency to:
  • CO2 hydrogenation to methanol and sustainable aviation fuel, and scale-up of Cu/ZIF-8.
  • Dry reforming and reforming of methane and crude oil to H2.
  • H2S decomposition to H2 and sulfur.
  • Methanol to hydrocarbons, oligomerization and alkylation to jet fuel.
  • Electrodes for CO2 reduction, microbial fuel cells, and microbial electrolysis cells.

Related People

Related Covers

Related Publications

Engineering Thermally Resistant Catalytic Particles for Oxidative Coupling of Methane Using Spray-Drying and Incorporating SiC

by Lezcano, Velisoju, Kulkarni, Ramirez, Castaño
Ind. Eng. Chem. Res. Year: 2021

Abstract

Oxidative coupling of methane (OCM) is a promising single-step route to convert natural gas to high-valued chemicals. It is generally agreed that Mn–Na–W catalysts offer a balanced conversion–selectivity trade-off. The present work outlines a novel SiC–SiO2 support synthesized by spray drying to extend the lifetime of the catalyst. Incorporating SiC into the support enables the exothermic reaction heat to be effectively dissipated, avoiding hotspots and thermal shocks, and increasing the thermal resistance. The spray drying technique yields particles with a consistent distribution of SiC inside the particles, amplifying the thermal resistance of the catalyst. Our kinetic results show that the spray dried catalyst with SiC has significantly higher stability at high C2selectivity compared to the benchmark SiO2-supported catalyst prepared by wetness impregnation. This result is due to (1) the more uniform distribution of active phases and SiC provided by the spray drying methodology and (2) the greater thermal resistance provided by SiC, which avoids thermal shocking and stabilizes the Mn–Na–W phases during the long-term (70 h) stability test for OCM.

Keywords

CHA HCE