Catalytic reactor engineering ⇒ information-driven design of packed (operando), fluidized, multi-functional, and -phase reactors


Reactor engineering (CRE)

Catalytic reactor engineering: information-driven design of packed (operando), fluidized, multifunctional and multiphase reactors. We design reactors that produce reliable, information-rich kinetic data with controlled hydrodynamics, and we use that information to scale reactors to pilot and industrial units. Prototypes are designed with our modeling workflow, verified in cold flow and then operated under reaction conditions.

Problem statement. At laboratory scale, a catalytic reactor should provide:

  • reliable kinetic information, with heat and mass transfer and hydrodynamics neglected or controlled;
  • a high data throughput, to accelerate model and catalyst discovery;
  • these results with the minimum use of reactants and generation of waste.

The pillars are quality, quantity and safety. In conventional laboratory reactors, conditions are kept steady, and the only way to obtain more information is miniaturization and parallelization [10, 18] . Very active catalysts, demanding chemistries and intensified processes need reactors that capture more information per experiment: dynamic as well as steady-state data, and the catalyst structure together with its performance. At pilot scale the objective changes to productivity, and the main difficulty is scale-up.

Our approach, scale by scale. The video starts at the industrial unit and ends with the data recorded in one experiment, and each paragraph below matches one scene.

1. Process: information decides the scale-up. Industrial reactors are designed from information obtained at small scale. In crude-to-chemicals, catalyst circulates between a regenerator and a fluidized reactor that converts crude oil into light olefins and aromatics in one step [104, 162] . The quality of the kinetic and hydrodynamic information decides how well such a unit can be scaled.

2. Scale-up: from centimeters to meters. We design reactor prototypes, test them in cold flow and scale them with CFD, CPFD and kinetics toward pilot and industrial units [171, 184] . With Saudi Aramco we developed the counter-current downer, a fluidized reactor between a riser and a co-current downer; counter-current operation increases solids holdup and breaks particle clusters [181, 211] . Patent applications on this design are in process. At pilot scale we seek industrial and investment partners.

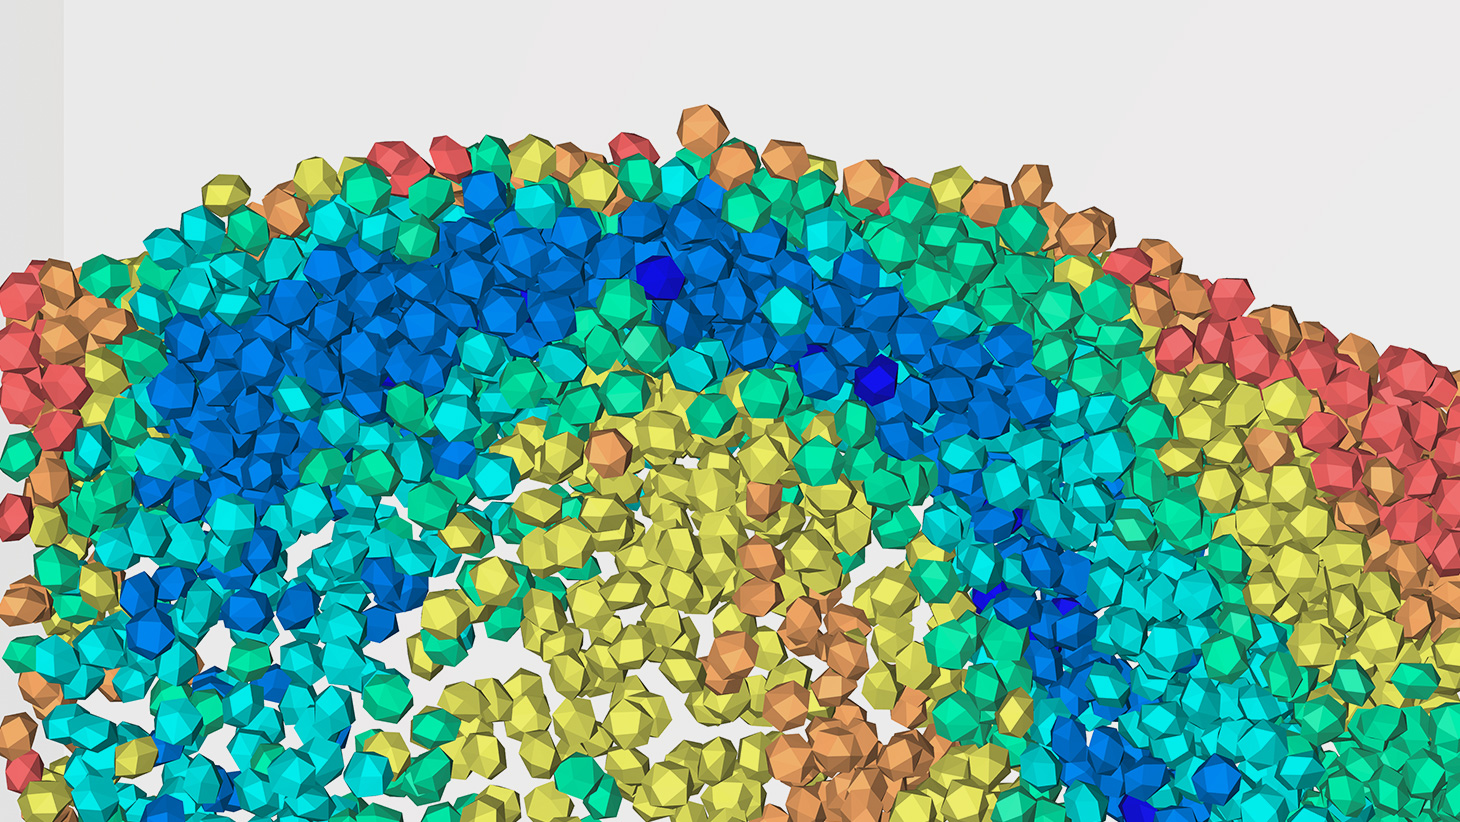
3. Lab reactors: designed for information. Our fluidized-bed laboratory visualizes and measures new reactor geometries with high-speed cameras, particle image velocimetry, optical probes, pressure transducers and dozens of fluidizable solids. The main laboratory reactors are:

  • CounterDowner, from micro-downer to scaled-up units [181, 184, 211] ;
  • CircuBED, a Berty-type reactor with internal recycle and circulating solids for intrinsic kinetics, in batch or continuous, packed or fluidized modes [120, 170] ;
  • multizone and diameter-transformed fluidized beds [104, 162, 209] ;
  • membrane reactors for pressurized H2 from ammonia [116] ;
  • multiphase reactors: trickle bed, slurry, micro-packed beds [24, 26, 84] and bioelectrochemical cells [174, 197] ;
  • photothermal reactors [189] ;
  • operando cells, where spectroscopy and kinetics are measured at the same time [124, 146] .

4. Operando cell: forcing the reactor. In packed-bed and operando reactors we change the conditions on purpose: pulses, step switches, isotope-labeled reactants (SSITKA), temperature and pressure cycles, and co-feeding of activity modifiers such as poisons or water [118, 160, 200, 205] . Infrared spectroscopy (DRIFTS) and mass spectrometry record how the surface and the products respond. We follow a spectro-kinetic, deactivation and hydrodynamic approach to resolve the individual steps [119, 124] .

5. Spectro-kinetics: one experiment, more information. Surface species and products are recorded together. Dynamic data separate fast and slow steps, give rate constants and deactivation rates, and check heat and mass transfer in the same experiment [118, 146] . This accelerates model and catalyst discovery, and feeds the multiscale models used for scale-up.

Goals. Our goals are grouped in these lines of work:

  • Multifunctional fluidized-bed reactors: multizone and circulating.
  • Packed-bed membrane reactors.
  • Forced dynamic reactors: pulsing and SSITKA.
  • Forced dynamic operando reactors: DRIFTS and TPSR.
  • Operando reactors.
  • Spray fluidized-bed reactors.
  • Downer reactor I: micro-downer.
  • Downer reactor II: counter-current operation and scale-up.
  • Batch Berty reactor for short contact times.
  • Multiphase reactors: trickle bed and slurry.
  • High-throughput experimentation (HTE) reactors.
  • Photothermal and bioreactors.
  • Reactor visualization and prototyping laboratory.
  • Spatio-temporal hydrodynamic characterization and validation.

Applications. We apply this competency to:
  • Crude-to-chemicals and fluid catalytic cracking, including co-cracking of plastics in a downer.
  • Short-contact-time reactors for crude-to-chemicals and crude-to-hydrogen, with a manufacturer for the new designs.
  • Dry reforming of methane and CO2 hydrogenation under forced dynamic conditions.
  • Ammonia decomposition in membrane reactors.
  • Bioelectrochemical reactors for wastewater treatment, H2 and electricity.

Related People

Related Covers

Related Publications

Hydrodynamic Characteristics of an Internal Recycle Berty Catalytic Reactor in Batch/Continuous or Packed/Fluidized Bed Modes

by Cui, Kulkarni, Wagner, Berger-Karin, Nagy, Castaño
ACS Eng. Au Year: 2022 DOI: https://doi.org/10.1021/acsengineeringau.1c00026

Abstract

Berty-type internal recycle reactors offer great opportunities for screening catalysts and reproducing catalytic reacting conditions in multiple processes, thus approaching industrial reactions while amplifying kinetic information. However, the rational design of these reactors requires a deeper understanding of their governing hydrodynamics and equations so that they can be better utilized in batch or continuous mode or as packed or fluidized beds. In this work, by adopting a slice model to represent a three-dimensional symmetric geometry with porous zone settings for catalyst beds, coupled with a species transport model, multiple reference frame, and SST k–ω turbulence model, we developed a computational fluid dynamic simulation strategy of a commercial Berty reactor manufactured by Integrated Lab Solutions (ILS). We conducted experiments to validate the proposed modeling approach under continuous packed bed operations, through which the hydrodynamic behaviors with packed/fluidized beds under the batch mode were also investigated by studying the influences of the transient injection, bed porosities, and rotation rates. As a result, we reported a set of equations to assess the bed velocity and contact time under different porosities, which simplified the performance improvements while replacing the need to perform complex simulations or conduct costly experiments. On the grounds of these hydrodynamic simulations and under various operating conditions, we discussed the pertinence of these instruments for intrinsic kinetic measurements in the batch/continuous or packed/fluidized bed operational modes.

Keywords

C2C FCC MKM CRE