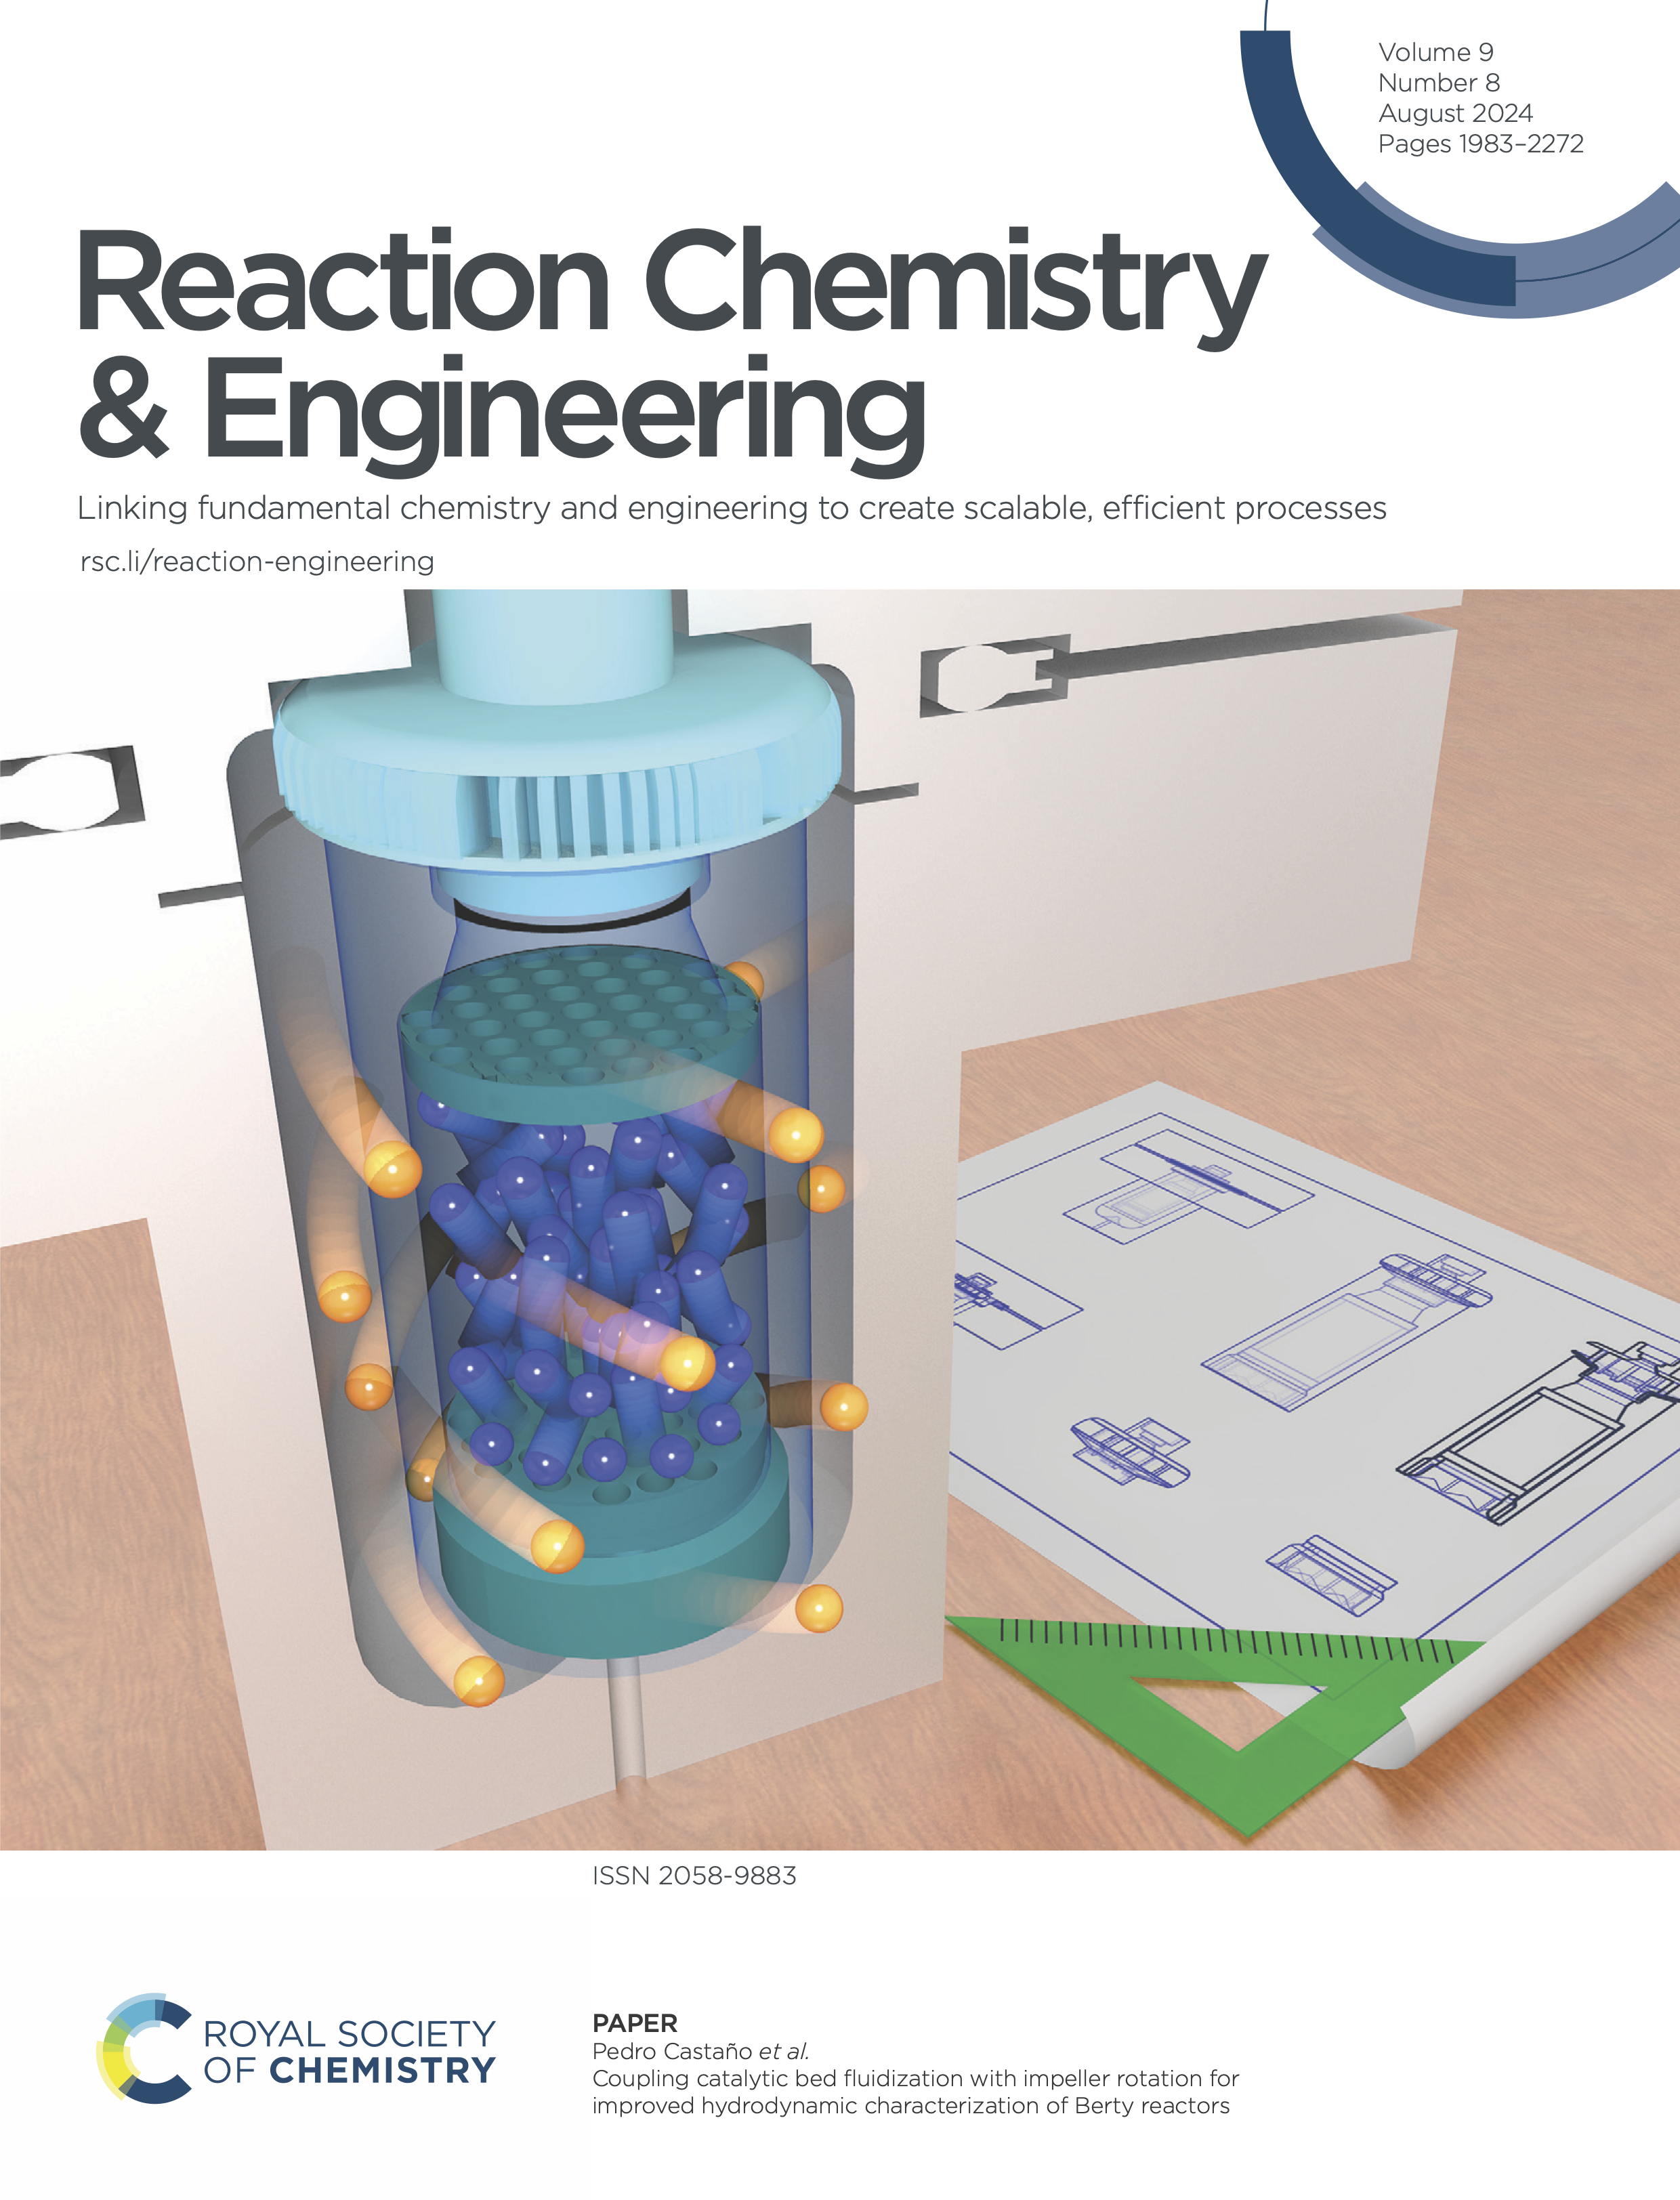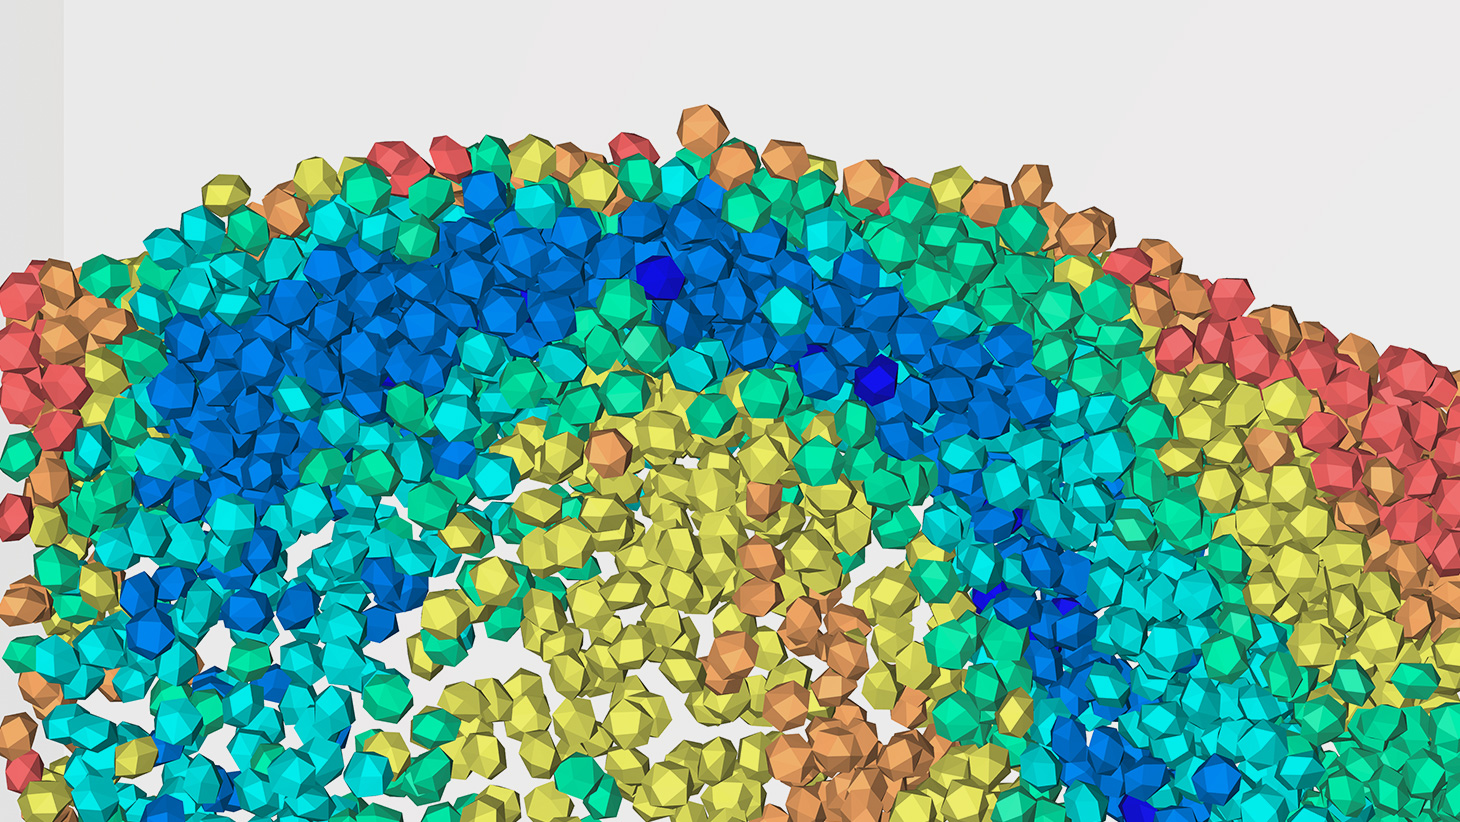
Catalytic reactor engineering: information-driven design of packed (operando), fluidized, multifunctional and multiphase reactors. We design reactors that produce reliable, information-rich kinetic data with controlled hydrodynamics, and we use that information to scale reactors to pilot and industrial units. Prototypes are designed with our modeling workflow, verified in cold flow and then operated under reaction conditions.
Problem statement. At laboratory scale, a catalytic reactor should provide:
The pillars are quality, quantity and safety. In conventional laboratory reactors, conditions are kept steady, and the only way to obtain more information is miniaturization and parallelization [10, 18] . Very active catalysts, demanding chemistries and intensified processes need reactors that capture more information per experiment: dynamic as well as steady-state data, and the catalyst structure together with its performance. At pilot scale the objective changes to productivity, and the main difficulty is scale-up.
Our approach, scale by scale. The video starts at the industrial unit and ends with the data recorded in one experiment, and each paragraph below matches one scene.
1. Process: information decides the scale-up. Industrial reactors are designed from information obtained at small scale. In crude-to-chemicals, catalyst circulates between a regenerator and a fluidized reactor that converts crude oil into light olefins and aromatics in one step [104, 162] . The quality of the kinetic and hydrodynamic information decides how well such a unit can be scaled.
2. Scale-up: from centimeters to meters. We design reactor prototypes, test them in cold flow and scale them with CFD, CPFD and kinetics toward pilot and industrial units [171, 184] . With Saudi Aramco we developed the counter-current downer, a fluidized reactor between a riser and a co-current downer; counter-current operation increases solids holdup and breaks particle clusters [181, 211] . Patent applications on this design are in process. At pilot scale we seek industrial and investment partners.
3. Lab reactors: designed for information. Our fluidized-bed laboratory visualizes and measures new reactor geometries with high-speed cameras, particle image velocimetry, optical probes, pressure transducers and dozens of fluidizable solids. The main laboratory reactors are:
4. Operando cell: forcing the reactor. In packed-bed and operando reactors we change the conditions on purpose: pulses, step switches, isotope-labeled reactants (SSITKA), temperature and pressure cycles, and co-feeding of activity modifiers such as poisons or water [118, 160, 200, 205] . Infrared spectroscopy (DRIFTS) and mass spectrometry record how the surface and the products respond. We follow a spectro-kinetic, deactivation and hydrodynamic approach to resolve the individual steps [119, 124] .
5. Spectro-kinetics: one experiment, more information. Surface species and products are recorded together. Dynamic data separate fast and slow steps, give rate constants and deactivation rates, and check heat and mass transfer in the same experiment [118, 146] . This accelerates model and catalyst discovery, and feeds the multiscale models used for scale-up.
Goals. Our goals are grouped in these lines of work:
Applications. We apply this competency to:
The optimal loading protocol of a microreactor (catalyst and inert: 0.1 mm, column: 2 mm internal diameter) with a catalyst–inert mixture is fundamentally different from that of a conventional lab-scale reactor (typical values: catalyst, 2 mm; inert, 0.2 mm; column, 10 mm internal diameter). This is shown to be due to segregation, occurring during loading. The following loading procedure has been used: premix the powders, funnel the mixture down, drop it within the reactor, and densify the bed. The average time a particle takes, from the mixing vial to reach its final position, depends on its properties, which in general results in an axially segregated bed. Radial segregation is observed for particles smaller than 60 m, as a result of electrostatic forces.
This paper describes for each handling step how to minimise segregation during the loading of a catalyst–diluent solid mixture. This includes using a funnel with a low-friction and steep wall, minimising difference in velocity of particle-gravity flow, and adding more inert after the mixture, prior to the densification step. The term is shown to sufficiently predict segregation due to the velocity difference during gravity flow. Segregation can be observed relatively easily in a glass mock-up reactor. Optimising all the handling steps to minimise segregation results in a visually homogeneous bed.