Multiscale kinetic modeling in catalysis ⇒ from microkinetics to computational fluid dynamics and process simulations


Multiscale modeling (MKM)

Multiscale kinetic modeling in catalysis: from microkinetics to computational fluid dynamics and process simulation. We connect models from the elementary step to the plant. Each scale passes parameters to the next, and design questions travel back down. Models are built together with the experiments of the other three competencies and are validated against them, so experiments are planned with the model, not guessed.

Problem statement. Catalytic processes occur at several scales at once: elementary steps on active sites, diffusion and heat transfer inside particles, hydrodynamics in the reactor and integration in the process. A model at one scale is not enough when the limiting phenomenon sits at another. Kinetic models fitted to limited or noisy data are not robust enough for scale-up.

We see multiscale modeling as the tool that links reaction understanding, catalyst and reactor design, scale-up and process optimization. We address each scale individually and the chain as a whole.

Our approach, scale by scale. The video zooms from the plant to the electrons, and each paragraph below matches one scene.

1. Process: the plant as a whole. Process models evaluate recycles, heat integration, energy use and scale-up scenarios. We use process system engineering (gPROMS and other packages) for ammonia crackers and reformers, including repurposing methane steam reformers as ammonia crackers [175], and for hydrocracking units, including techno-economic analysis [148]. These models need a reliable reactor model inside.

2. Reactor: flow, heat and solids. We couple hydrodynamics, heat transfer and kinetics in computational fluid dynamics:

  • CFD (Ansys Fluent) for gas-solid packed beds and operando cells [124] ;
  • CPFD (Barracuda) for fluidized beds, downers and risers, validated with particle image velocimetry [162, 181, 184] ;
  • dimensionless and reactor models for membrane reactors producing pressurized, high-purity H2 from ammonia [116, 142] .

3. Particle: reaction against transport. Inside each particle, reaction competes with diffusion and heat transfer. This determines how much of the catalyst actually works. Particle models connect intrinsic kinetics with the shaped catalyst, including the effect of SiC and of the shaping method [190], and population balances describe how particles grow during shaping [204].

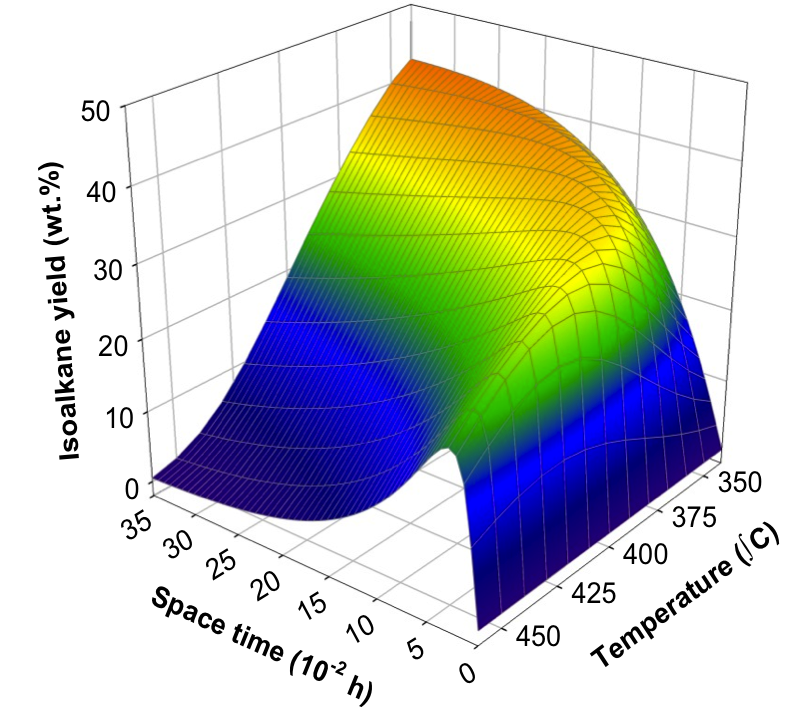
For complex feeds, macrokinetic models (lumped and empirical) are often the most robust choice. They detect changes in mechanism, optimize conditions and support reactor pre-design. We make them robust with:

  • lumping and continuous lumping strategies for crude-to-chemicals cracking and plastic-oil hydrocracking [177, 195, 206] ;
  • acidity descriptors and lumped models for methanol to hydrocarbons and aromatics [156, 176] ;
  • neural networks combined with DFT for reforming kinetics [117] ;
  • outlier detection and data curation for large datasets from high-throughput reactors [154] .

4. Surface: microkinetics. Microkinetic models resolve the rate of each elementary step, the rate-determining step, and adsorption and desorption, with thermodynamic constraints imposed [168] . Langmuir-Hinshelwood and Eley-Rideal formulations are used where they apply. We applied this approach to promoters and active sites in:

  • Ga on Cu for CO2 hydrogenation to methanol [127, 191] ;
  • K on Ru and Ba on Co-Ce for ammonia decomposition [140, 147] ;
  • microscopic SiC on Mn-Na2WO4/SiO2 for oxidative coupling of methane [190] ;
  • Ni in hollow ZSM-5 for ethylene oligomerization [198] ;
  • sulfide catalysts for H2S dissociation, using reaction descriptors [180] .

5. Electrons: DFT. Density functional theory (DFT) supplies adsorption and barrier energies, supports the assumed pathways and provides initial parameter estimates [140, 180] . From here, parameters move up the chain to the process, and design questions move back down.

Goals. Our goals are grouped in these lines of work:

  • Microkinetics I: key thermodynamic relationships and thermodynamic consistency.
  • Microkinetics II: fitting, training and optimization against kinetic and spectroscopic data.
  • Microkinetics III: ab initio kinetic modeling with DFT energies and reaction descriptors.
  • Macrokinetics: complex reaction networks and population balances.
  • CPFD: fluidized reactor modeling and scale-up.
  • CFD: reactor modeling and optimization.
  • CFD II: modeling operando reactors, to separate kinetics from transport and hydrodynamics.
  • Process system engineering: gPROMS models for scale-up, intensification and techno-economic evaluation.

Applications. We apply this competency to:
  • Ammonia cracking and crude-to-chemicals with Saudi Aramco: multiscale kinetic models guided scale-up to pilot plant in both projects.
  • CO2 hydrogenation, reforming and oxidative coupling of methane.
  • Hydrocracking of refractory, renewable and waste streams.
  • Design of new fluidized and operando reactors, together with the reactor engineering team.

Related People

Related Covers

Related Publications

One-step conversion of crude oil to light olefins using a multi-zone reactor

by Alabdullah, Rodriguez Gomez, Shoinkhorova, Dikhtiarenko, Chowdhury, Hita, Vittenet, Sarathy, Castaño, Bendjeriou-Sedjarari, Abou-Hamad, Zhang, Ali, Morales-Osorio, Xu, Gascon
Nat. Catal. Year: 2021

Abstract

With the demand for gasoline and diesel expected to decline in the near future, crude-to-chemicals technologies have the potential to become the most important processes in the petrochemical industry. This trend has triggered intense research to maximize the production of light olefins and aromatics at the expense of fuels, which calls for disruptive processes able to transform crude oil to chemicals in an efficient and environmentally friendly way. Here we propose a catalytic reactor concept consisting of a multi-zone fluidized bed that is able to perform several refining steps in a single reactor vessel. This configuration allows for in situ catalyst stripping and regeneration, while the incorporation of silicon carbide in the catalyst confers it with improved physical, mechanical and heat-transport properties. As a result, this reactor–catalyst combination has shown stable conversion of untreated Arabian Light crude into light olefins with yields per pass of over 30 wt% with a minimum production of dry gas.

Keywords

C2C HCE MKM CRE