Catalytic reactor engineering ⇒ information-driven design of packed (operando), fluidized, multi-functional, and -phase reactors


Reactor engineering (CRE)

Catalytic reactor engineering: information-driven design of packed (operando), fluidized, multifunctional and multiphase reactors. We design reactors that produce reliable, information-rich kinetic data with controlled hydrodynamics, and we use that information to scale reactors to pilot and industrial units. Prototypes are designed with our modeling workflow, verified in cold flow and then operated under reaction conditions.

Problem statement. At laboratory scale, a catalytic reactor should provide:

  • reliable kinetic information, with heat and mass transfer and hydrodynamics neglected or controlled;
  • a high data throughput, to accelerate model and catalyst discovery;
  • these results with the minimum use of reactants and generation of waste.

The pillars are quality, quantity and safety. In conventional laboratory reactors, conditions are kept steady, and the only way to obtain more information is miniaturization and parallelization [10, 18] . Very active catalysts, demanding chemistries and intensified processes need reactors that capture more information per experiment: dynamic as well as steady-state data, and the catalyst structure together with its performance. At pilot scale the objective changes to productivity, and the main difficulty is scale-up.

Our approach, scale by scale. The video starts at the industrial unit and ends with the data recorded in one experiment, and each paragraph below matches one scene.

1. Process: information decides the scale-up. Industrial reactors are designed from information obtained at small scale. In crude-to-chemicals, catalyst circulates between a regenerator and a fluidized reactor that converts crude oil into light olefins and aromatics in one step [104, 162] . The quality of the kinetic and hydrodynamic information decides how well such a unit can be scaled.

2. Scale-up: from centimeters to meters. We design reactor prototypes, test them in cold flow and scale them with CFD, CPFD and kinetics toward pilot and industrial units [171, 184] . With Saudi Aramco we developed the counter-current downer, a fluidized reactor between a riser and a co-current downer; counter-current operation increases solids holdup and breaks particle clusters [181, 211] . Patent applications on this design are in process. At pilot scale we seek industrial and investment partners.

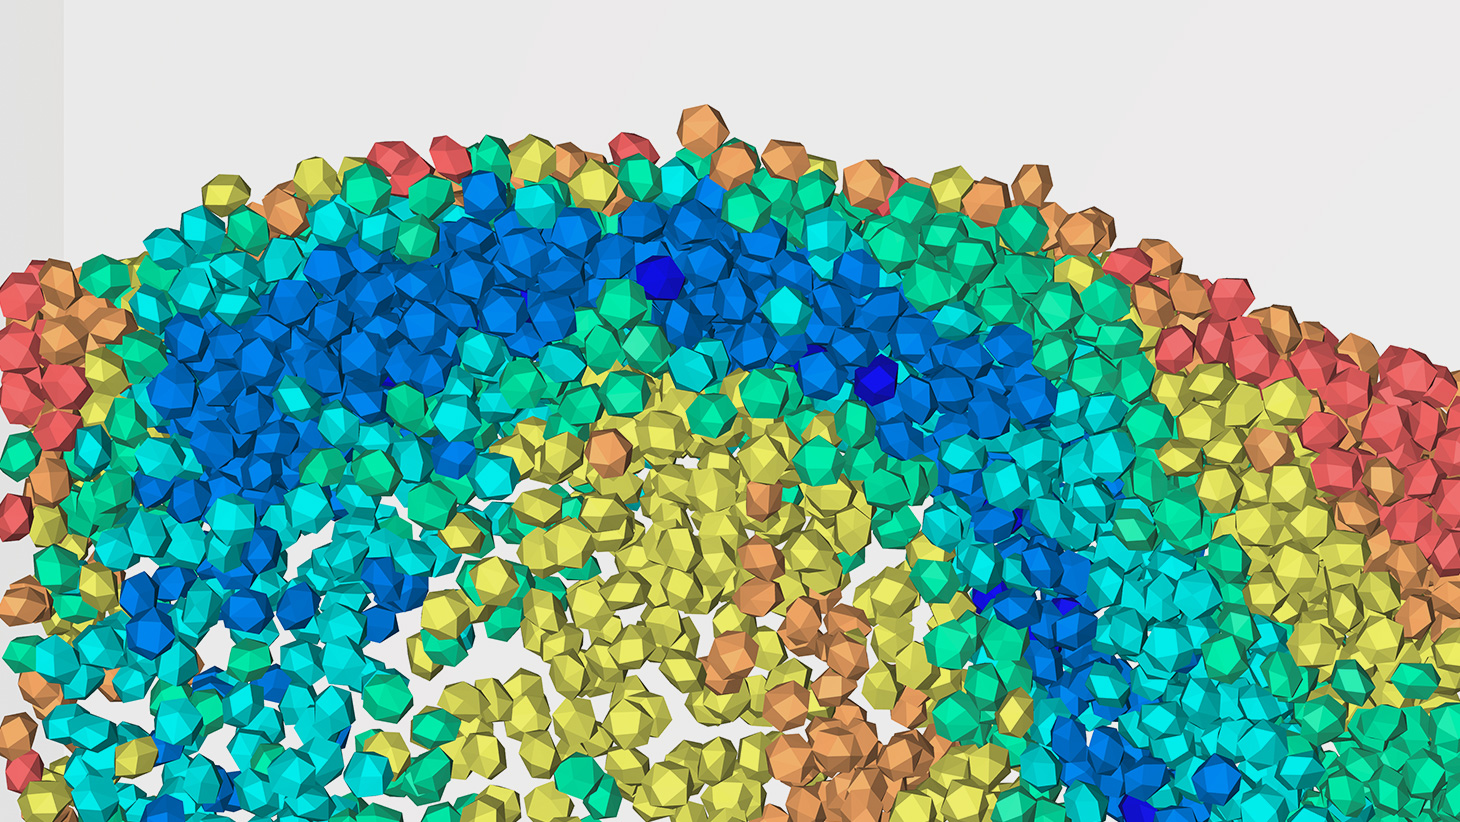
3. Lab reactors: designed for information. Our fluidized-bed laboratory visualizes and measures new reactor geometries with high-speed cameras, particle image velocimetry, optical probes, pressure transducers and dozens of fluidizable solids. The main laboratory reactors are:

  • CounterDowner, from micro-downer to scaled-up units [181, 184, 211] ;
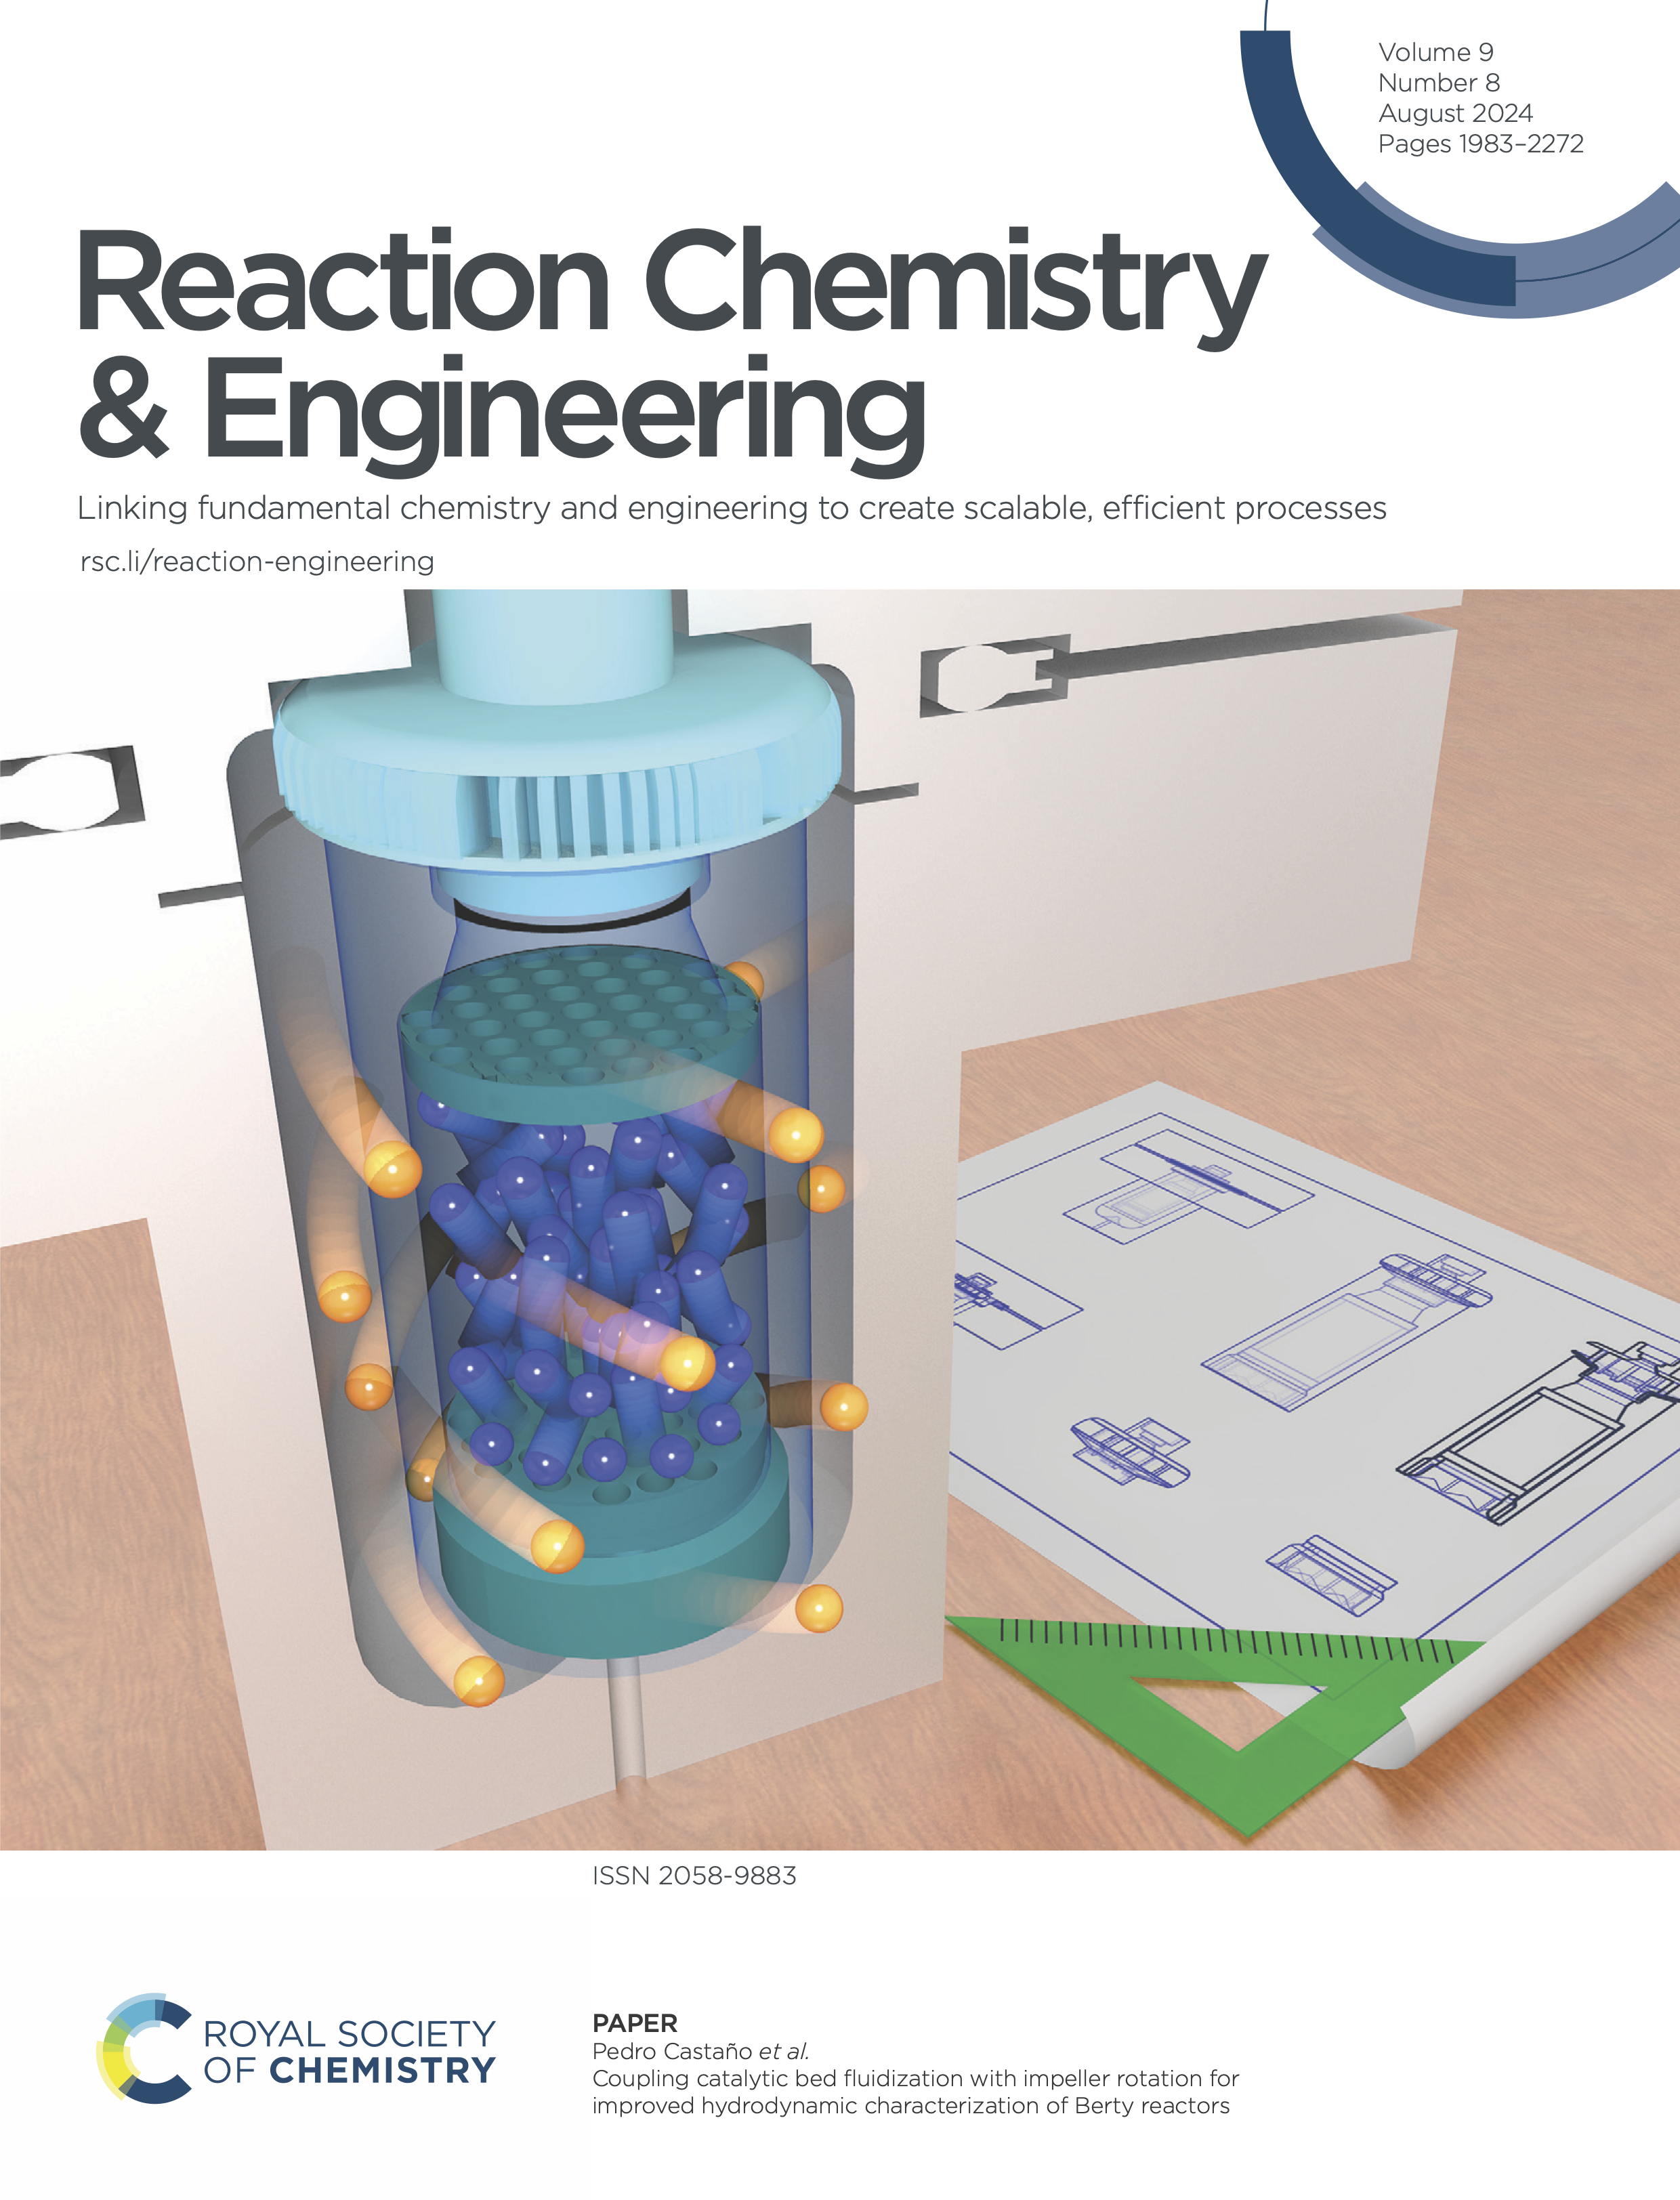
  • CircuBED, a Berty-type reactor with internal recycle and circulating solids for intrinsic kinetics, in batch or continuous, packed or fluidized modes [120, 170] ;
  • multizone and diameter-transformed fluidized beds [104, 162, 209] ;
  • membrane reactors for pressurized H2 from ammonia [116] ;
  • multiphase reactors: trickle bed, slurry, micro-packed beds [24, 26, 84] and bioelectrochemical cells [174, 197] ;
  • photothermal reactors [189] ;
  • operando cells, where spectroscopy and kinetics are measured at the same time [124, 146] .

4. Operando cell: forcing the reactor. In packed-bed and operando reactors we change the conditions on purpose: pulses, step switches, isotope-labeled reactants (SSITKA), temperature and pressure cycles, and co-feeding of activity modifiers such as poisons or water [118, 160, 200, 205] . Infrared spectroscopy (DRIFTS) and mass spectrometry record how the surface and the products respond. We follow a spectro-kinetic, deactivation and hydrodynamic approach to resolve the individual steps [119, 124] .

5. Spectro-kinetics: one experiment, more information. Surface species and products are recorded together. Dynamic data separate fast and slow steps, give rate constants and deactivation rates, and check heat and mass transfer in the same experiment [118, 146] . This accelerates model and catalyst discovery, and feeds the multiscale models used for scale-up.

Goals. Our goals are grouped in these lines of work:

  • Multifunctional fluidized-bed reactors: multizone and circulating.
  • Packed-bed membrane reactors.
  • Forced dynamic reactors: pulsing and SSITKA.
  • Forced dynamic operando reactors: DRIFTS and TPSR.
  • Operando reactors.
  • Spray fluidized-bed reactors.
  • Downer reactor I: micro-downer.
  • Downer reactor II: counter-current operation and scale-up.
  • Batch Berty reactor for short contact times.
  • Multiphase reactors: trickle bed and slurry.
  • High-throughput experimentation (HTE) reactors.
  • Photothermal and bioreactors.
  • Reactor visualization and prototyping laboratory.
  • Spatio-temporal hydrodynamic characterization and validation.

Applications. We apply this competency to:
  • Crude-to-chemicals and fluid catalytic cracking, including co-cracking of plastics in a downer.
  • Short-contact-time reactors for crude-to-chemicals and crude-to-hydrogen, with a manufacturer for the new designs.
  • Dry reforming of methane and CO2 hydrogenation under forced dynamic conditions.
  • Ammonia decomposition in membrane reactors.
  • Bioelectrochemical reactors for wastewater treatment, H2 and electricity.

Related People

Related Covers

Related Publications

Evaluating performance of vortex-diode based hydrodynamic cavitation device scale and pressure drop using coumarin dosimetry

by Sarvothaman, Kulkarni, Subburaj, Hariharan, Velisoju, Castaño, Guida, Prabhudharwadkar, Roberts
Chem. Eng. J. Year: 2024 DOI: https://doi.org/10.1016/j.cej.2024.148593

Abstract

The present work investigates the hydrodynamic cavitation (HC) performance of vortex-diode based devices, which show early inception and superior cavitational performance compared to conventional devices. The study provides novel data on the cavitational efficiency at different operating pressures for two sizes of cavitation devices, addressing a gap in the literature. Using coumarin as a chemical dosimeter in acidic conditions, the study tracked the formation of 7-hydroxycoumarin (7OHC), a hydroxylation product of coumarin, to evaluate cavitational performance. Optimization of solution pH and initial concentration led to selecting pH 3 and a 15 ppm concentration for subsequent experiments with two vortex-diode devices of 12 mm (D12) and 6 mm (D6) diameters. These devices were tested under various pressure conditions. The formation of 7OHC was analyzed in relation to process time, number of passes, and a characteristic number of passes (n*) – which correlates device dimensions with operating velocity. The results indicated that the D6 device outperformed the D12 in terms of efficiency at inlet pressures ranging from 100 to 400 kPag. Analysis of 7OHC formation trends with respect to n* revealed that while there were variations within different pressures for a given device, the performance was comparable across different scales. By keeping a constant n* across varying pressures (P1 = 100 to 400 kPag and P2 = 0 to 300 kPag), the study observed comparable 7OHC formation across different operating conditions and scales. This data is vital for selecting suitable scales and conditions for HC devices and for validating multi-scale models in this field.

Keywords

CRE